



Injection molding and 3D printing do not have a universal volume threshold where one always becomes cheaper. For a B2B project, compare the same released part, material requirement, finish, inspection and delivery scope using supplier quotes. The break-even quantity depends on those inputs, the mold investment and the recurring cost of each qualified part.
This guide gives buyers a like-for-like comparison method, a project-specific break-even formula and a validation checklist for choosing between injection molding, additive manufacturing or a staged combination of both.
Compare the full project scope
| Cost or requirement | Injection molding | 3D printing |
|---|---|---|
| One-time and setup costs | Tool design and manufacture, trials, sampling and any qualification work. | Build preparation, machine setup or fixtures, support strategy and any process qualification required by the project. |
| Recurring part cost | Quoted resin, cycle and machine assumptions, labor, yield, inspection, finishing and packaging. | Quoted machine time and material plus supports, post-processing, finishing, inspection and packaging. |
| Lead time | Tool design/build, sample trials, corrections and production release. | Machine availability, build time, post-processing, inspection and shipping for the selected process. |
| Geometry and design | Parting line, pull direction, draft, gates, ejection and any side actions or other tool features. | Build direction, support or powder removal, feature resolution, joining and process-specific post-processing. |
| Part performance | Validate the selected resin grade, flow, weld lines, geometry, dimensional results and intended service conditions. | Name the additive process, feedstock/resin, build orientation and post-processing; validate the finished part in its intended load case. |
“3D printing” covers different processes, and “injection molded” does not describe a single resin grade or part result. Compare named material and process data, drawing revision, tolerances, surface requirements, inspection, order schedule and delivery basis. For polymer material-extrusion parts specifically, NIST research describes how weld-zone behavior can vary with printing conditions; do not generalize one process result to every additive technology. Autodesk’s draft-angle guidance explains how mold pull direction, texture, geometry and material affect ejection planning.
References: NIST research on material-extrusion weld zones and Autodesk Moldflow draft-angle guidance.
Calculate a project-specific break-even quantity
First separate one-time costs from recurring cost per acceptable part. A simple comparison is:
Injection molding total = molding setup and tooling + quantity × molded-part cost
Additive manufacturing total = additive setup + quantity × printed-part cost
When additive manufacturing has the higher recurring part cost, the estimated crossover is:
Break-even quantity = (molding setup/tooling − additive setup) ÷ (printed-part cost − molded-part cost)
Include the same scope in both per-part numbers: material, machine time, yield or scrap assumptions, finishing, inspection, packaging and delivery. If the printed-part recurring cost is not higher, or one option does not meet the required function, the formula will not produce a useful switch point for that project. Recalculate when geometry, material, order size or process changes.
Illustrative calculation—not a market benchmark
Assume only for demonstrating the arithmetic that an additive quote is $8 per acceptable part, the molded-part quote is $0.60 per acceptable part, the molding tool and setup total $6,000, and additive setup is $0. Under those hypothetical inputs:
Break-even = $6,000 ÷ ($8 − $0.60) ≈ 811 parts.
This is not a typical industry crossover or a supplier price. Replace every input with current quotes for the same part and scope. A different tool, build process, finish, material, batch schedule or inspection requirement can move the answer substantially.
Compare design and part performance by process
| Question | What to establish for injection molding | What to establish for additive manufacturing |
|---|---|---|
| Will the part meet its load case? | Test the named resin grade, part geometry, gate/flow assumptions, weld lines and any fiber orientation that matters. | Name the print process, material, build orientation and post-processing. Test the finished part in the required load direction and environment. |
| Can the geometry be produced? | Review draft, pull direction, parting line, ejection, wall transitions and the cost/maintenance of any slides or lifters. | Review build orientation, support removal or powder evacuation, minimum features, surface, joining and finishing. |
| Will dimensions and finish be acceptable? | Define critical dimensions and tolerances after tool trials; confirm measurement method and cavity/sample plan. | Define the same drawing requirements and measurement method; account for build and post-processing steps in the acceptance sample. |
Do not describe molded parts as automatically isotropic or every printed part as weak across layers. Material, process, geometry and build conditions matter. Compare a representative finished sample against the same functional, dimensional and appearance requirements.
Choose a route for the project stage
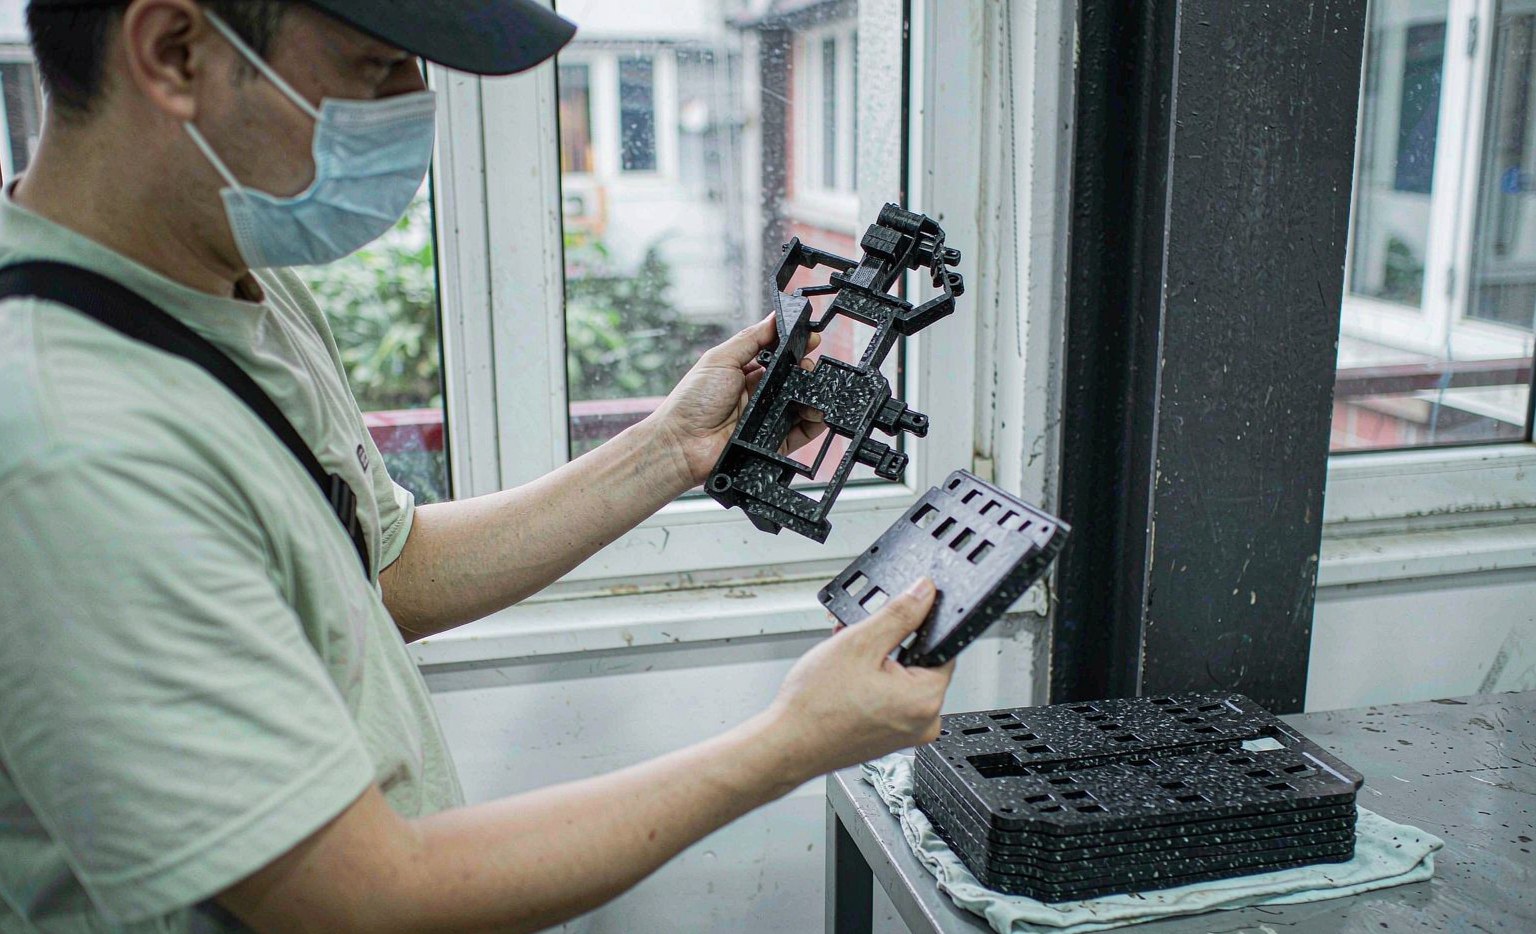
- Consider additive manufacturing when the design is changing, the quantity is limited, a tool is not yet justified, or the chosen process can make a geometry that suits the project. Include post-processing and any performance qualification in the quote.
- Consider injection molding when the design and resin are sufficiently defined, repeat production is planned, and the quote shows that tooling and qualification can be amortized over the required demand.
- Consider a staged plan when a printed prototype or bridge batch can support validation while tooling and production samples are prepared. Define the approved transition point and whether the printed and molded versions meet the same requirements.
Do not release production merely because a CAD model is printable or moldable. Check the production drawing, test results, approved material/process, inspection plan and revision control for the chosen route.
What to request in comparable RFQs
- Part drawing and revision, annual demand, order quantity, ramp schedule and required ship dates.
- Material grade and color; surface/appearance requirements; critical dimensions and functional load case.
- For molding: tool scope, tool ownership and maintenance, cavity plan, trial/approval milestones and quoted cycle assumptions.
- For additive: specific process and machine/material, build orientation, batch layout, supports, post-processing and inspection assumptions.
- For both: part price at each order quantity, expected yield, inspection, packaging, freight, exclusions and change-control charges.
- Sample acceptance plan, validation responsibility, applicable quality records and production-release approval.
For the mold-design and material details that affect the comparison, use DAYIN’s injection-molding DFM guide, ABS, PP and PC resin comparison and injection-molding RFQ cost guide. For a project quote, review the custom injection-molding service or send DAYIN the drawing and annual volume.
Frequently asked questions
At what volume should I switch from 3D printing to injection molding?
There is no universal quantity. Compare the one-time molding investment and setup with additive setup and like-for-like recurring costs, then calculate the crossover for the exact part, process, finish and demand plan.
Is a 3D-printed plastic part as strong as an injection-molded part?
There is no process-wide answer. Results depend on the additive technology, material, build orientation and post-processing, and on the molded resin grade, geometry and flow. Test representative finished parts against the same load and service requirements.
Can I mold a 3D-printed design directly?
Review it for the mold’s pull direction, draft, parting line, ejection and any undercuts. Some geometry may need design changes or additional tool features before it can be molded.
Does mold tooling cost rise directly with part size?
Part size and complexity can change tool design, steel, machine and handling requirements, but the quote depends on the specific tool scope. Compare itemized quotes rather than applying one multiplier.
Can 3D printing be used for bridge production?
It can be evaluated for a limited batch while tooling is prepared if the selected process, material, function, finish and acceptance plan meet the project requirements. Agree the transition criteria before launch.
Should post-processing be included in the process comparison?
Yes. Include the finishing, dimensional inspection, cleaning, assembly or other operation required for an acceptable delivered part in each route’s quoted scope.